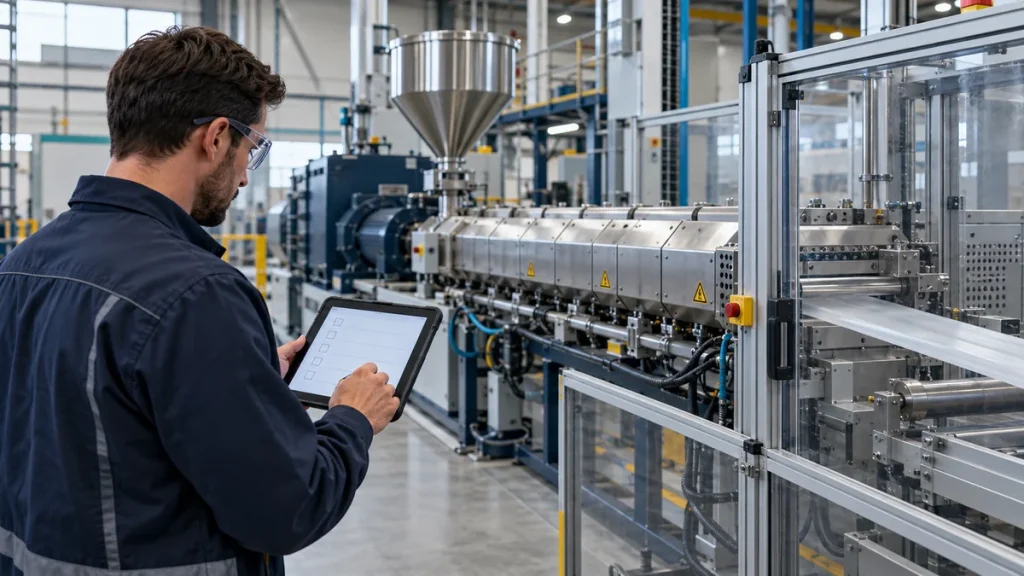
A factory acceptance test, or FAT, is most useful when the buyer and supplier agree what the test must demonstrate before it begins. For plastic machinery, that means connecting the equipment scope, representative material and product requirements to a written record. A video of a running line is useful context, but it does not replace an acceptance plan.
Agree the basis before the visit
List the machine identifiers, quotation revision, drawings and technical requirements that will be reviewed. Mark which equipment is physically included in the test and which will be checked through a different method. Record the authorized participants and who can resolve a disputed observation.
SGS describes FAT around contractual requirements, functionality, completeness and documentation. Use those categories to organize the agenda, then write project-specific questions beneath them. A general inspection template should not silently introduce conditions that the parties never agreed to test.
Create a test matrix
| Requirement | Evidence to agree |
|---|---|
| Equipment identity and scope | Nameplate records, configuration list and scope comparison |
| Material trial | Feed batch identity, preparation history and recorded conditions |
| Output acceptance | Sampling method, test method and agreed evaluation criteria |
| Handover documents | Document index, revision status and outstanding-item owner |
Separate a measured result from an observer’s comment. If an instrument reading is important to acceptance, identify the instrument and the relevant measurement record. If the plant cannot demonstrate a requirement at the factory, document the limitation and agree the later verification route.
Protect the meaning of the material trial
Identify the feed before the run and label the output samples so they can be traced back to the test. Record any pre-treatment, formulation change or equipment substitution. The report should make clear whether the demonstrated conditions represent the buyer’s intended operation.
Ask the supplier to explain the approved operating sequence and the safety conditions for the demonstration. Qualified personnel should conduct any required functional or protective-system checks using agreed procedures. Buyers should observe and record evidence without improvising tests on operating machinery.
Manage exceptions as decisions
Use a punch list that states the requirement, observation, supporting record, responsible person and proposed resolution. Distinguish an incomplete test from a failed result. Neither should disappear into a general “accepted with comments” sentence that does not explain the consequence.
Agree how corrections will be verified and how final acceptance will be documented under the project’s terms. Keep the relevant drawings, sample records and approved changes with the final report. A concise, traceable exception is more actionable than a long unstructured list of photographs.
Separate FAT from shipment checks
Pre-shipment inspection has a different emphasis, including verification of goods and shipment readiness within the agreed inspection scope, as described by TÜV SÜD. Confirm the equipment, packing references and document package against the shipment plan. Do not assume a successful running trial proves that the complete package is ready to dispatch.
Our factory audit and inspection service can be discussed around your agreed evidence requirements. For the next project stage, review shipping and export coordination and installation and training preparation so the handover responsibilities are clear.